Precision Turned Parts for EV Charging Connectors

An EV charging connector is a small part with a large job. It has to seat against a plug thousands of times, hold a seal in rain and dust, carry current without heating up, and look like it belongs on a forecourt. Most of that is decided by a lathe and a finishing line.
What the connector body has to do
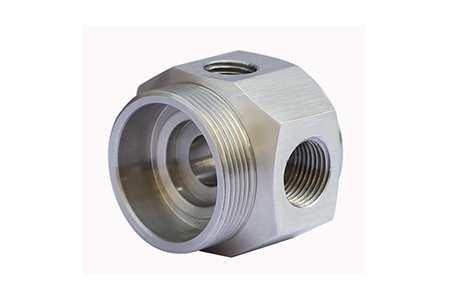
The body carries the contact, centers the mating plug, and holds the seal that keeps water out of the terminal chamber. Three features do most of the work: the bore that locates the contact, the seal land that sets compression, and the thread or collar that locks the connection. Each has its own tolerance, and the way they stack is what determines whether the plug inserts smoothly or binds at the last few millimeters.
6061-T6 is the usual alloy for the shell: free-machining, stable, and receptive to anodizing. Where a part needs more wear resistance at the contact seat, a stainless insert or a different alloy is specified for that feature alone.
Turning strategy and tolerance stack
Bore, seal land and thread are turned in one setup wherever the geometry allows, because every re-chuck adds runout between features that must be concentric. Bar stock is chosen close to finished diameter to keep the number of passes down and the thermal load low. Seal lands get a dedicated finishing pass with a small nose radius, since surface texture there matters more than dimensional class.
Long, thin shells deflect. Where wall thickness drops below a few millimeters, we support the bore with a mandrel or turn between centers rather than accepting a taper that inspection will find later. The same logic applies to turned and milled connector components with a seal at both ends.
Anodizing that survives outdoor service
Type II anodizing gives color and corrosion resistance, but it also grows the surface and can close a thread or a seal land if the masking plan is careless. Threads, seal lands and electrical contact faces are masked before anodizing; everything that mates is left bare or finished to its own specification.
Color match matters on a forecourt. We work to a sample or a color reference and keep parts from one batch together through the line, because anodizing shade shifts with bath age and part position.
Inspection before shipment
Bore diameter, seal land diameter and surface finish, thread gauge, concentricity between bore and seal land, coating thickness on the anodized areas, and a visual check on color and masking. Parts ship in trays that protect the finished surfaces, because a scratched connector is a rejected connector. Finishing and tolerance questions are collected in our FAQ.
Prototype quantities for connector redesigns are usually small, and the schedule is set by a certification test rather than by a production plan. That suits the way we work. Start a connector project with a drawing and a target test date.
Writer: Rosie Zou
WhatsApp: +86 138 2729 4028
Email: rosiezou@k-tekmachining.com
Customer Some Samples